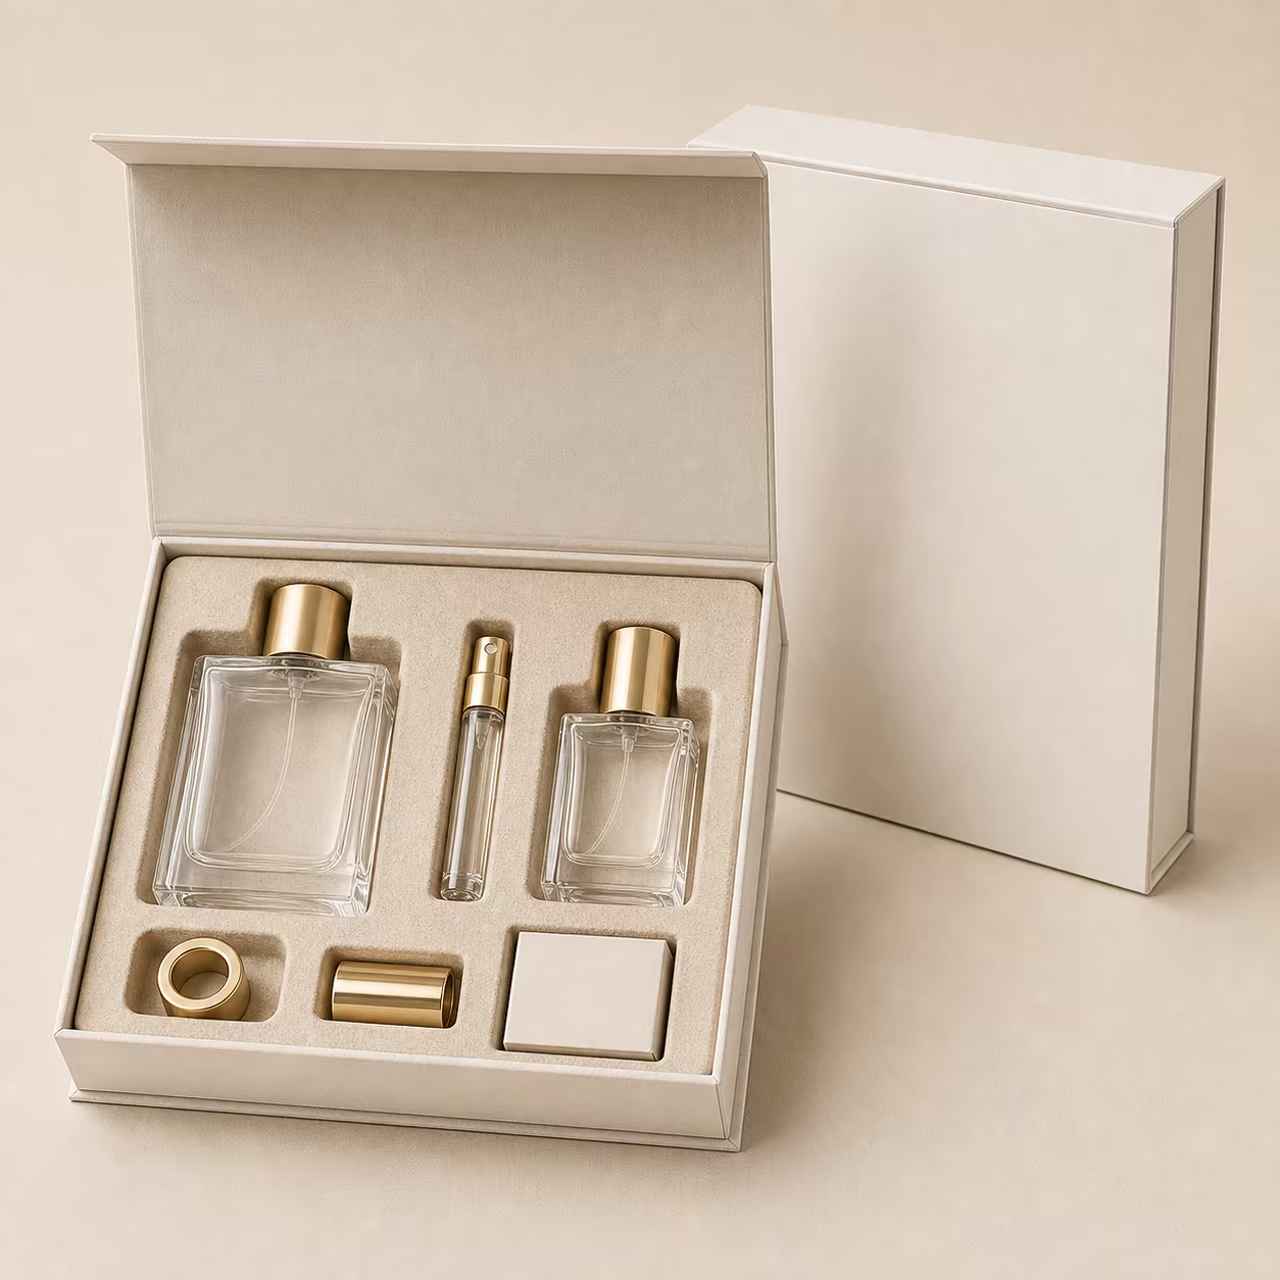
Molded pulp packaging inserts can hold fragrance bottles, skincare jars, grooming sets and discovery kits while supporting a fiber-based presentation. They are not an automatic replacement for foam or a thermoformed plastic tray. The right insert depends on product fragility, weight, geometry, surface finish, removal action, retail presentation, shipping route and the recovery system addressed by any environmental claim.
Start with the protection problem rather than a preferred material story. A heavy glass bottle with a decorative cap creates different loads from a flexible tube set or an aluminum tin. The insert, retail box and export or ecommerce pack must work together; a tight presentation cavity alone does not prove distribution performance.
Map the product and likely failure modes
Record the production-intent dimensions, weight, center of gravity, protruding components and vulnerable surfaces. Identify what must not happen: glass-to-glass contact, cap release, pump actuation, label scuffing, coating abrasion, movement, crushing or an unpresentable opening experience. Include every component in a kit and the order in which the buyer should remove it.
Decorated bottles can be slightly larger than blank reference parts. Coating, labels, sleeves and tolerances can change fit, while an insert designed too tightly can pull off a cap or mark a soft-touch finish. Build the prototype around final or representative decorated components and define clearance at critical points.
Understand molded-pulp design limits
Molded pulp uses fiber slurry formed and dried in tooling. Tool access, draft, wall transitions, radii, thickness, drying and trimming influence the finished cavity. Deep undercuts, sharp cosmetic edges and extremely tight tolerances may be difficult or require a different structure. Ask whether the project uses transfer-molded, thermoformed or another pulp process because surface and precision can vary.
Review dust, loose fiber, odor, moisture response, color variation and surface smoothness with the product. A natural texture may support the design, but fine fragrance finishes or optical components may need contact protection. Tissue wraps, paper bands or localized pads can help, provided the added material and assembly steps are included in the approved system.
Compare alternative insert structures
Folded paperboard can create clean printable panels and ship flat, but tabs, creases and locking features need enough strength for the product. Corrugated or honeycomb structures can add cushioning and compression support for heavier items, although exposed edges may not deliver the desired retail appearance.
Foam can provide cushioning, low dust and precise cavities for fragile products, but resin type, density, adhesives, recovery route and brand requirements need review. Thermoformed plastic trays can offer repeatable geometry, visibility and nesting, while gauge, color, static, scuff risk and local recycling context affect the decision. A hybrid may place a presentation insert inside a separate protective shipper instead of forcing one layer to perform every function.
Design fit, access and unboxing together
Check cavity depth, side clearance, finger notches, product orientation and the force needed to remove each item. A package should restrain the product during transit without asking a customer to pry against a pump, cap or glass edge. Keep required labels, shade names and instructions visible at the right step.
Turn, shake and open prototypes as a customer would. Look for product migration, components hiding under the insert, torn pulp edges and loose accessories. Assembly teams also need a repeatable loading sequence and a way to confirm every cavity is filled before the outer box closes.
Test the complete packed system
Conditioning, compression, vibration and drop evaluation should reflect the intended distribution environment and final packed configuration. ASTM D4169 provides a framework for evaluating shipping units against distribution hazards, but the responsible team must choose the assurance level, sequence and acceptance criteria for the project.
Inspect both functional and visual outcomes. A bottle may remain unbroken while its cap loosens, label scuffs or premium coating becomes unacceptable. Test the retail box inside the actual ecommerce mailer or export carton with final void fill, dividers, orientation and pallet assumptions. Retest when the bottle weight, insert material, box board or packing arrangement changes.
Assess humidity, storage and assembly
Fiber structures can respond to moisture and prolonged compression. Review performance after relevant humidity and temperature conditioning, stacked storage and the expected assembly timeline. Define acceptable warping, cavity recovery, surface marks and odor. Protect unfinished inserts from uncontrolled warehouse exposure before packing.
Record tooling ownership, cavity version, fiber composition, color, drying or finishing route, tolerance, nesting quantity and packing method. Samples from a prototype tool may not represent production texture or stiffness exactly, so identify which sample is approved for appearance and which production-intent trial validates performance.
Make environmental claims from the whole system
A fiber insert may reduce one type of plastic, but it can also require added wraps, adhesives, coatings or a larger box. ISO 18602 frames packaging optimization around maintaining required functions while reducing weight or volume. ISO 18604 and FTC guidance reinforce that recycling or environmental claims need conditions and substantiation rather than a material name alone.
Compare the complete packaging bill of materials against a defined baseline, including the retail box and shipping protection. State the insert material accurately, identify coatings or laminations, and qualify recovery claims for the destination context. The best choice is the lightest practical system that protects the product, supports assembly and use, and allows the brand to make narrow claims it can defend.
Protective insert material comparison
Choose the insert from the product, presentation and distribution functions. Material category alone does not establish protection, recyclability or a lower environmental impact.
| Insert route | Useful direction | Qualification focus |
|---|---|---|
| Molded pulp | Fiber-based formed cavities for bottles, jars, grooming sets and premium kits. | Draft, radii, fit tolerance, dust, moisture, scuff contact, nesting and production texture. |
| Folded paperboard | Printable flat structures, dividers and presentation platforms for moderate loads. | Tab and crease strength, assembly, cavity retention, edge contact and shipping protection. |
| Corrugated or honeycomb | Cushioning and compression support for heavier or more fragile products. | Flute or cell direction, cut edges, movement, visual finish, humidity and carton integration. |
| Foam | Precise cushioning and surface contact for selected fragile or high-finish products. | Resin and density, dust, odor, adhesives, compression set, scuffing and recovery route. |
| Thermoformed plastic | Repeatable geometry, visibility and nested trays for component sets. | Resin, gauge, static, sharp edges, scuffing, cavity fit, label area and local recovery context. |
| Hybrid system | Presentation insert combined with wraps, pads, dividers or a separate protective shipper. | Complete bill of materials, assembly time, pack volume, interaction and distribution evidence. |
Selection considerations
Compare molded pulp with paperboard, corrugated, foam, thermoformed plastic and hybrid structures against the same product and route. Model production-intent decorated components, then assess fit, removal, scuffing, humidity, assembly and distribution inside the final retail and shipping pack. Material category alone does not prove protection or recyclability.
Questions to resolve before sampling
- Which fragility, weight, vulnerable finish, movement and removal requirements must the insert control?
- How do molded pulp, paperboard, corrugated, foam, thermoformed plastic or a hybrid compare for the complete pack?
- What conditioning, compression, vibration, drop, assembly and environmental-claim evidence is needed before approval?
What to send with an inquiry
Share the application or formula, capacity, material preference, closure or dispensing component, decoration, estimated quantity, destination country, target timing and any reference drawings or photos. Final specifications, MOQ, availability and testing requirements are confirmed for the selected configuration.
Primary references and scope
- ASTM D4169 distribution testing overview — Provides a framework for evaluating shipping units against distribution hazards.
- ISO 18602:2013 packaging-system optimization overview — Describes assessment of packaging weight or volume while preserving required packaging functions.
- ISO 18604:2013 material-recycling overview — Defines assessment requirements for packaging intended to be recoverable through material recycling.
- FTC environmental claims summary — Explains qualification and substantiation considerations for recycled-content, recyclable and refillable claims in the U.S.
- ISO 14021:2026 environmental claims overview — Describes requirements and guidance for self-declared environmental statements used on products, packaging and digital materials.
These sources support distribution planning, packaging optimization and environmental-claim frameworks; they do not certify a molded-pulp insert, guarantee protection or establish local recycling access. Test the production-intent product, insert, retail pack and export or ecommerce carton together.